Why operator training pays off on the shop floor
In glass and plastic marking, a small setup mistake can show up immediately as a faint code, a missed logo or a mark that sits a few millimetres off position. That is why training is not a nice extra. It is part of keeping production stable. A well-trained operator knows how to check product position, confirm the right file is loaded, and spot a change in beam focus before it becomes a batch problem.
For factories working under tight schedules, especially where changeovers are frequent, training also cuts downtime. Teams do not have to call for help every time a format changes or a line stops for a short break. They understand what to check first, which saves time and protects output. In our experience, the strongest plants are usually the ones where the operator at the machine can make sensible decisions without guessing.
What good training should cover from day one
Proper training goes beyond pressing start. The operator must understand the material, the mark, and the setting that sits behind it. Glass behaves differently from plastics, and different plastic grades can react very differently to heat, speed and energy. If that is not explained early, the team will spend time chasing inconsistent results.
- How to load and secure product so the mark lands in the same position every time
- How to check focus, mark contrast and line speed before a production run
- How to load the correct file and confirm the right job parameters
- How to recognise early signs of poor alignment or poor part presentation
- How to clean basic surfaces and keep dust away from the mark area
- How to follow safety steps around laser equipment and enclosed work areas
These basics may sound simple, but they prevent many of the errors we see on busy lines. A machine can only repeat what it is given. If the setup is poor, the marking will be poor too.
Training that protects consistency across shifts
One of the most common problems in South African production is shift-to-shift variation. The morning operator sets up carefully, the afternoon shift makes a few adjustments and by the night run the mark has drifted. That is where structured training has real value. Everyone follows the same method, uses the same checks and records the same results.
When staff know what to measure and what to ignore, mark consistency improves over time. This matters for traceability, branding and customer confidence. It also helps maintenance teams because they can see whether a fault is mechanical, software related or simply the result of a change in handling. The better the training, the less guesswork is needed later on.
- Use a standard setup sheet for every shift
- Keep sample parts from approved runs for comparison
- Record parameter changes instead of relying on memory
- Train more than one operator for each line
- Review rejected parts weekly, not only when there is a complaint
A local example from Jet Park to a production line in Boksburg
We often see the difference training makes in the Ekurhuleni industrial area. A packaging company in Boksburg, for example, may run clear plastic components during the day and switch to a darker material later on. If only one person understands the settings, every absence creates pressure. But when the team is trained properly, the line keeps moving even if the supervisor is pulled into another meeting or the power returns after load-shedding and the machine must be restarted.
In that kind of setup, the operator learns how to confirm the file, check the part orientation, and test a sample before full production resumes. That saves material and avoids rework. It also gives the business better control over output when deadlines are tight and the plant is working through a hot, dusty week or a humid coastal delivery schedule that affects handling and storage.
At our Jet Park base, we see this pattern often enough to know it is not theory. Training gives teams confidence, and confidence reduces mistakes.
Why hands-on training beats a quick handover
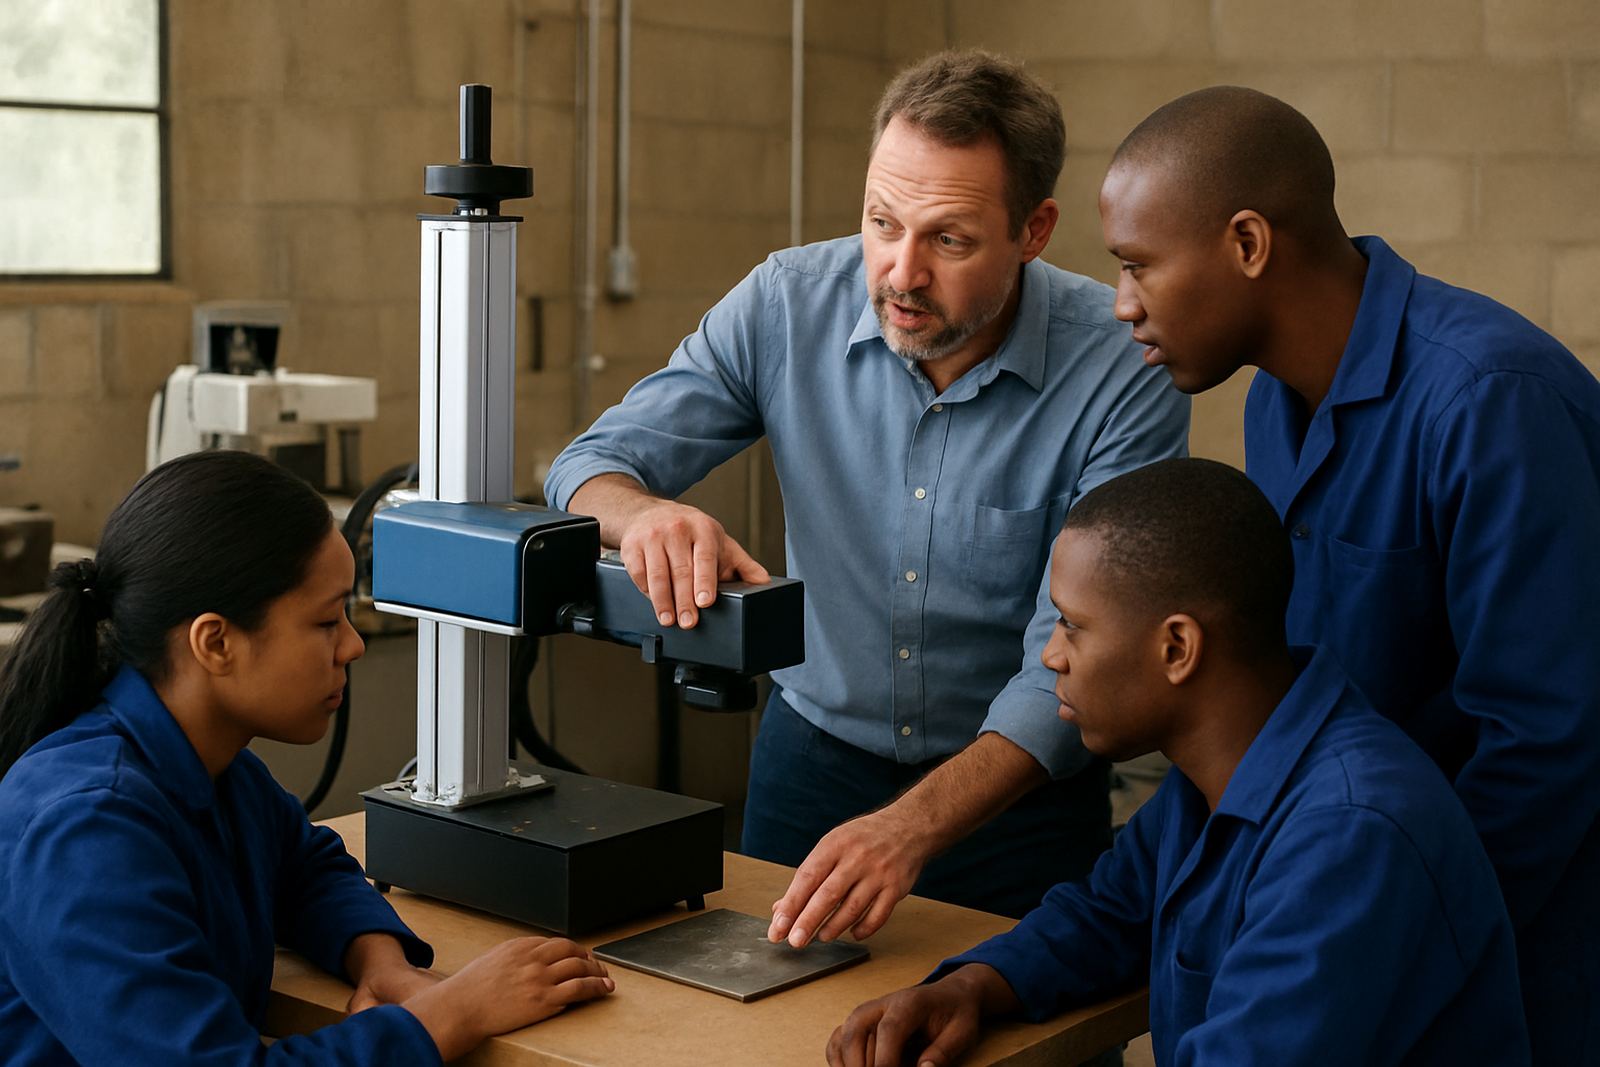
A short handover may get the machine running, but it rarely gives operators the judgement they need when something changes. Hands-on training lets staff see the effect of small adjustments, ask questions, and learn what good results look like on the actual product they handle every day. That is far better than a rushed briefing after installation.
Our training approach is practical and tied to the real production environment. We work through the job files, sample marks and line conditions the team will actually face. That includes fixture use, handling, cleaning, and the steps needed to keep the mark clear and permanent. When staff learn on their own parts and own line, the lesson sticks.
- Training on live or sample product, not only theory
- Clear steps for setup, fault checks and restart procedures
- Guidance for new staff and refresher support for existing teams
- Notes that can be kept near the machine for quick reference
Keeping skills current after installation
Training should not end once the machine is commissioned. Staff change, production needs grow and product lines often shift. A team that was well prepared last year may need a refresh when a new item is introduced or when a process is modified. Regular follow-up keeps standards steady and helps prevent bad habits from settling in.
For businesses in Germiston, Kempton Park, Benoni, Alberton, Midrand and Pretoria, this is especially useful when one site runs multiple shifts or sends work between lines. A small refresher can save hours later. It is also worth scheduling training after preventive maintenance or software changes, because even a familiar system can behave differently after a service intervention.
The goal is simple: fewer errors, cleaner marks and less waste. When operators understand the process, the marking system becomes a reliable part of production instead of a point of frustration.
What to ask before booking operator training
Before arranging training, it helps to be clear about the line, the material and the result you need. That gives the trainer a proper starting point and helps the session focus on the real challenges your team faces. A good programme should be practical, repeatable and easy for supervisors to support after the visit.
- What material are you marking, and how often does it change?
- How many operators need training on each shift?
- Do you need help with file setup, fixture design or line integration as well?
- Are there quality issues linked to setup errors, rework or slow changeovers?
- Would a site demo, sample testing or refresher visit help your team most?
When the right questions are asked early, the training is more useful from the start. That is usually the difference between a line that keeps drifting and a line that holds its mark from week to week.