Why batch code planning matters on a busy line
In many South African factories, the batch code is doing more work than people realise. It is not just a mark on a bottle, lid, tub or panel. It ties product to a run date, shift, machine setting, material lot, and sometimes a customer or export requirement. When the code is planned badly, staff waste time checking artwork, correcting the wrong date, or stopping the line to fix a mistake that should never have reached production.
Good planning keeps the marking step simple. The operator knows what code goes where, the supervisor can sign off faster, and the quality team has a clean record if there is a complaint later. On a fast-moving line in Jet Park or Germiston, that can save a surprising amount of time over a week.
It also reduces risk. A code that is too small, too close to a mould line, or placed on a curved surface can be hard to read and harder to scan. If you supply packaging, medical items, household goods or component parts, you need a code that stays legible after handling, washing, stacking, or transport.
Start with the product, not the code text
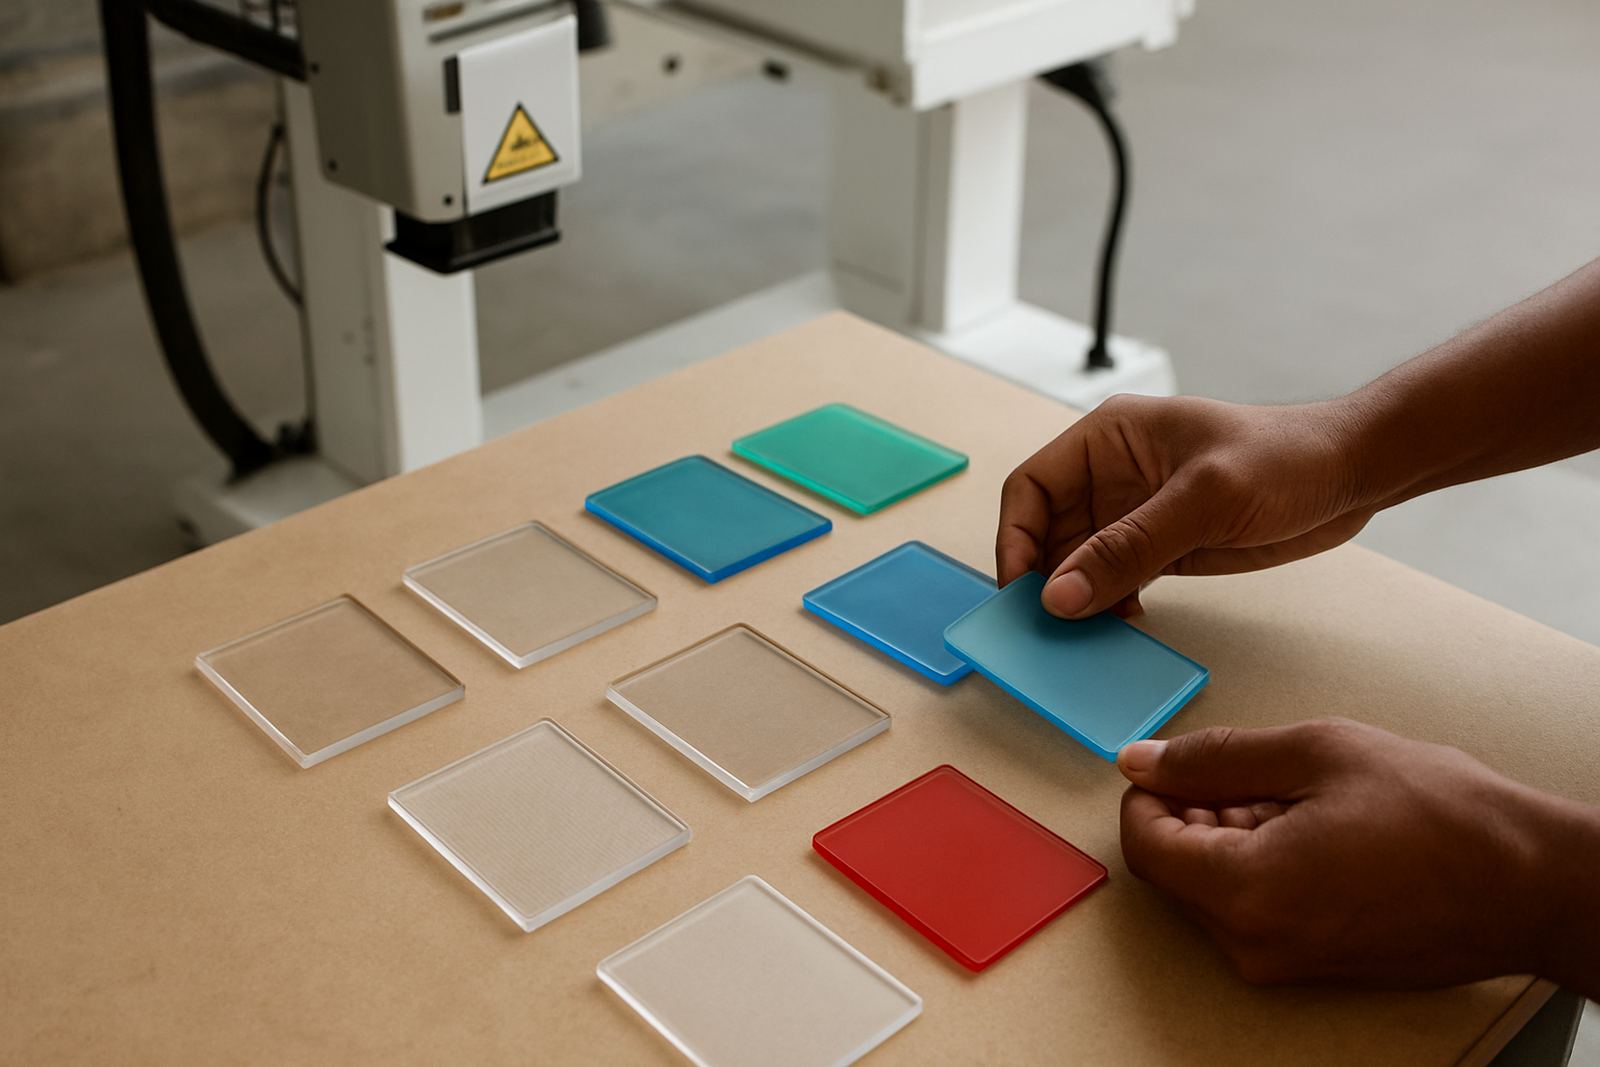
The first question is not what the code should say, but where it will sit and how the material behaves. Glass and plastic do not mark the same way. Thickness, colour, transparency, gloss, and curvature all affect readability. A clear bottle, a black ABS part, and a soft-touch plastic cap need different settings and sometimes a different position on the product.
Before finalising the code format, look at the following points:
- Surface type and finish, such as gloss, matte, ribbed or curved
- Available marking area and how much space is needed for a readable code
- Product speed on the line and whether marking happens in motion or at a stop
- Heat, dust and moisture in the production area, especially near coastal humidity or open loading bays
- Whether the mark must be visible to the eye, readable by scanner, or both
Once that is clear, the code format can be set properly. That might include production date, line number, shift, cavity, or a short internal reference. Keep it simple enough for operators to enter without confusion. The more complicated the code, the more likely someone will type the wrong suffix or date format.
Build a code format that operators can use under pressure
In practice, a good batch code is one that can be used the same way every day. Operators should not need to guess whether the month comes before the day, or whether the shift code changes with the weekend schedule. A clear format helps across different teams, and it makes training much easier when there is staff turnover.
A useful code format usually follows a fixed structure. For example, a plant may decide that every mark must carry the product family, date and shift, then add a short internal sequence number when needed. If one site in Benoni uses a different format from a site in Pretoria, the team should still be able to read it at a glance. Standardisation is what saves time.
When planning the format, ask these questions:
- Will the code be changed manually or pulled from production software
- Does the team need a daily, weekly or monthly reset
- Is the code for internal traceability only, or must it meet customer or export rules
- Will the same format work on both glass and plastic products
It helps to test the format with real staff before launching it. A code that looks neat on a screen may be awkward on the line, especially during a night shift or after a power interruption.
Match the marking method to the job
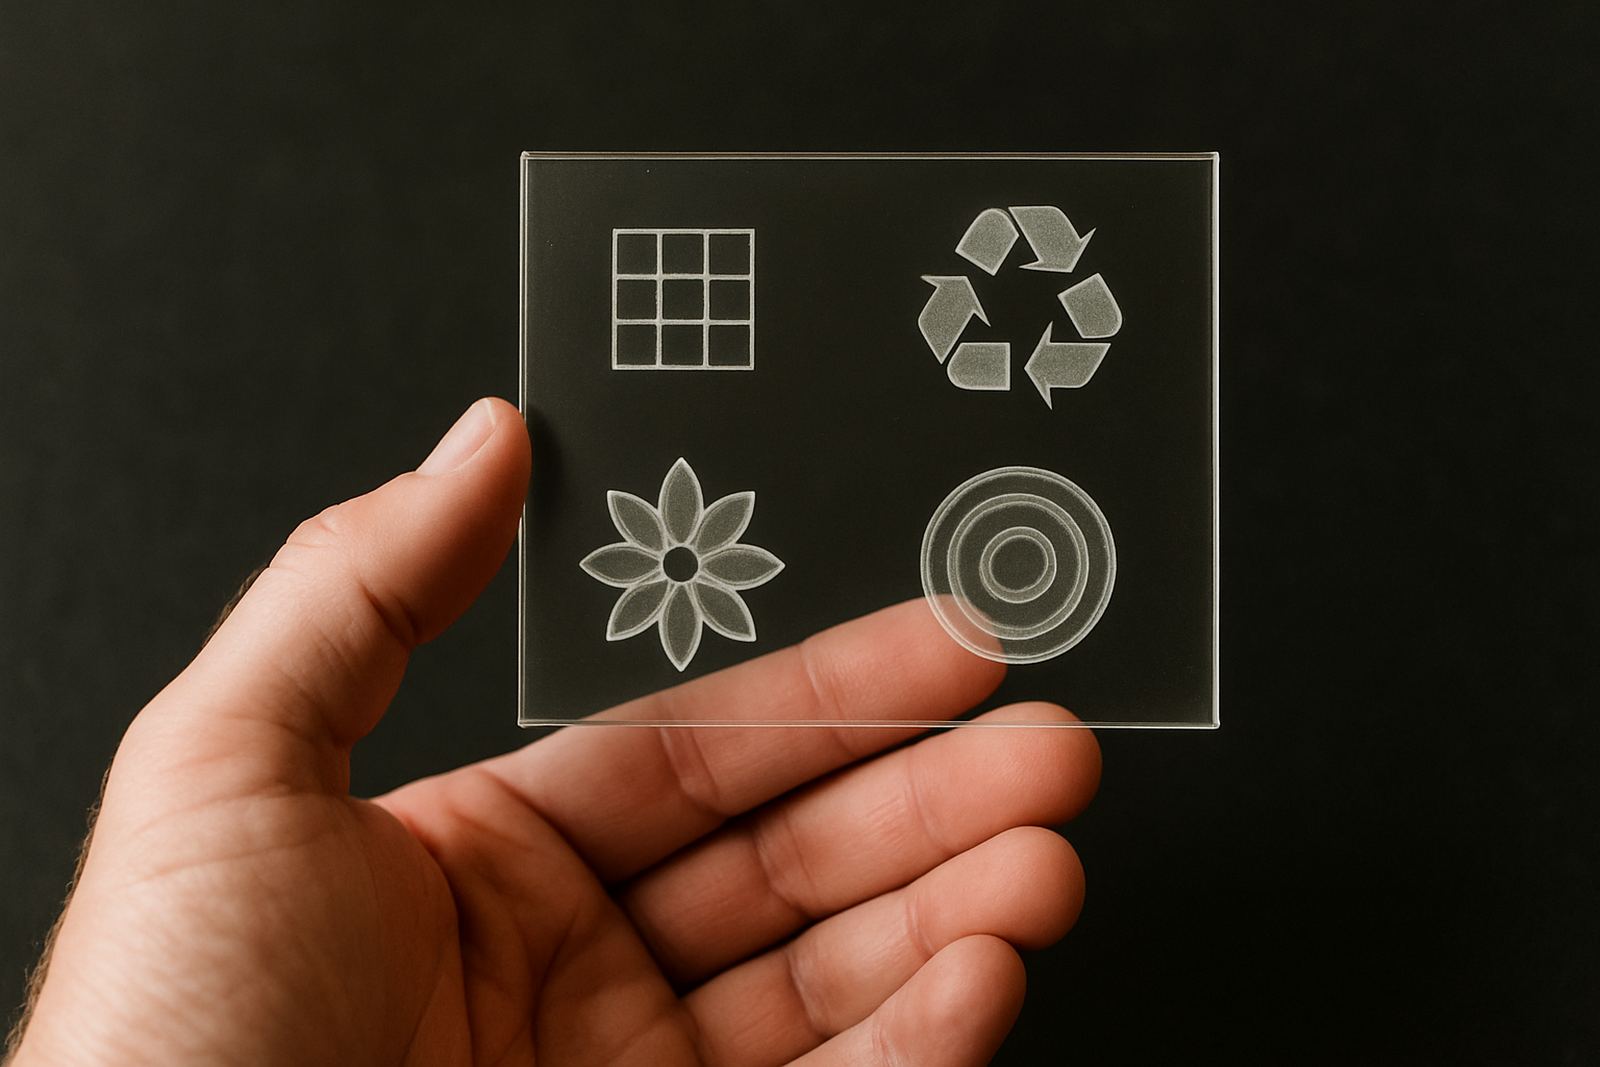
Batch code planning is not only about the code itself. The marking method must suit the product, the pace of the line and the quality expected. For glass and plastics, permanent laser marking is often preferred where a durable mark is needed without inks, solvents or labels that can peel. That is useful on items that are washed, handled often, or exposed to heat and friction.
Laser marking also suits plants that want a clean finish and repeatable results. Once the settings are correct, the mark can stay consistent from run to run. That said, the mark still depends on good planning. If the code area is too small or the product moves too much during marking, even a good system can produce poor results.
On site, the team should check:
- Mark contrast on the actual material, not only on a sample sheet
- Code placement so it does not interfere with moulding, assembly or scanning
- Cycle time so the line does not wait for the marking step
- Integration with fixtures, sensors or conveyor movement if the line is automated
In Ekurhuleni, where many factories run mixed shifts and tight dispatch windows, the ability to keep marking stable through long production days is often just as important as the code format itself.
Plan for changeovers, not just steady production
Many batch code problems happen during changeovers. The previous run ends, a new order is released, and somebody updates the code in a hurry. If the process has no clear sequence, the wrong date or product code can go straight onto the next batch. That is a costly mistake, especially when the line is producing large volumes.
A strong planning process includes a simple changeover routine. The code should be checked against the job card, the operator should confirm the new format before the first run, and the first marked samples should be inspected before full production starts. This is basic, but it prevents a lot of rework.
Useful changeover controls include:
- A signed code change checklist
- A reference sample for each approved code format
- Named responsibility for release of the first article
- A clear rule for who may edit the code settings
- Spare fixtures or settings saved for repeat jobs
When daily production is tight, these checks might feel like extra steps. In reality they save time because they stop the line from running with the wrong code. That is better than trying to sort out cartons or pallets later.
Keep traceability useful, not cluttered
Traceability only helps if the code can be read and linked back to something meaningful. Some factories overload the mark with too much detail. That may look thorough, but it can make the code difficult to read on small parts or reflective surfaces. Better to mark the minimum information needed for traceability and keep the rest in the production record.
For many South African businesses, the ideal setup is a short code on the product itself, backed by a job sheet or digital record that stores the fuller details. That gives the quality team enough information without overcomplicating the mark. If a customer asks for proof of production, the record should match the code exactly.
Good batch planning also helps with recalls or complaints. If one shift had a problem, the business should be able to isolate the affected run quickly. That is where clear code structure and consistent setup matter. It is a practical safeguard, not a paperwork exercise.
Get the line ready for steady marking in South Africa conditions
Local conditions matter more than many teams expect. Dust, vibration, temperature swings and power interruptions can all affect consistency. In some areas, load-shedding means equipment needs to recover cleanly after a stop, with the code settings intact and the team able to restart without confusion. Near the coast, moisture can also affect certain materials and fixtures, so the marking plan should be tested in the real environment, not only in a clean room.
Before settling on a batch coding setup, it helps to run sample testing on the actual product and inspect the results under normal lighting. If a code is meant to be read by staff on the floor, it should still be visible when the product is moving past a conveyor or stacked for dispatch. If it is meant for scanning, test that too.
In Jet Park, Boksburg and surrounding industrial areas, many teams want a system that can handle mixed production without creating more admin. The best results usually come from a combination of clear code planning, practical operator training, and a marking setup that fits the line rather than forcing the line to adapt around it.