Why plastic barcodes fail when the spacing is wrong
Plastic is a tricky surface because it changes with moulding, texture and colour. A code that looks fine on the screen can become hard to read once it sits on a curved cap, a ribbed housing or a glossy panel, and that is where spacing starts to matter. If the bars are too close together, the scanner sees them as one block. If they are too far apart or too shallow, the code looks weak and may not hold up after transport, cleaning or contact with oils.
In practice, barcode suitability on plastic is about the full part, not only the marking point. Wall thickness, surface finish, pigment and the size of the label area all affect the result. On a moulded component in Jet Park or a packaging line in Benoni, the same code that works on one part may need adjustment on another. That is why sample testing is worth doing before a full run, not after the first batch has already left the line.
- Keep the code large enough for the available scan distance.
- Leave a clear quiet zone around the barcode.
- Avoid placing the mark over seams, corners or mould lines.
- Test the code on the actual plastic grade, not a similar sample.
Choose the right barcode size for the part
There is no single size that suits every plastic item. Small parts need compact codes, but a code that is too small will force the operator or scanner to work harder. Larger parts can carry bigger codes with better contrast and easier scan rates. The aim is to make the barcode readable at normal line speed without taking over the product face.
On flat panels, a neat rectangular mark is often enough. On smaller caps, cosmetic containers or technical housings, the barcode may need to move to a side wall or underside where there is more room. For plastic parts used in warehouses around Germiston or Kempton Park, it also helps to think about the reader itself. Handheld scanners, fixed scanners and camera systems all have different tolerances, so the code size should match the equipment already in use.
- Use a code format that fits the data you need to carry.
- Check the minimum character height before marking production stock.
- Allow extra space if the part has a curve or texture.
- Confirm the scan from the same angle operators will use on site.
Permanent marking methods that suit plastics
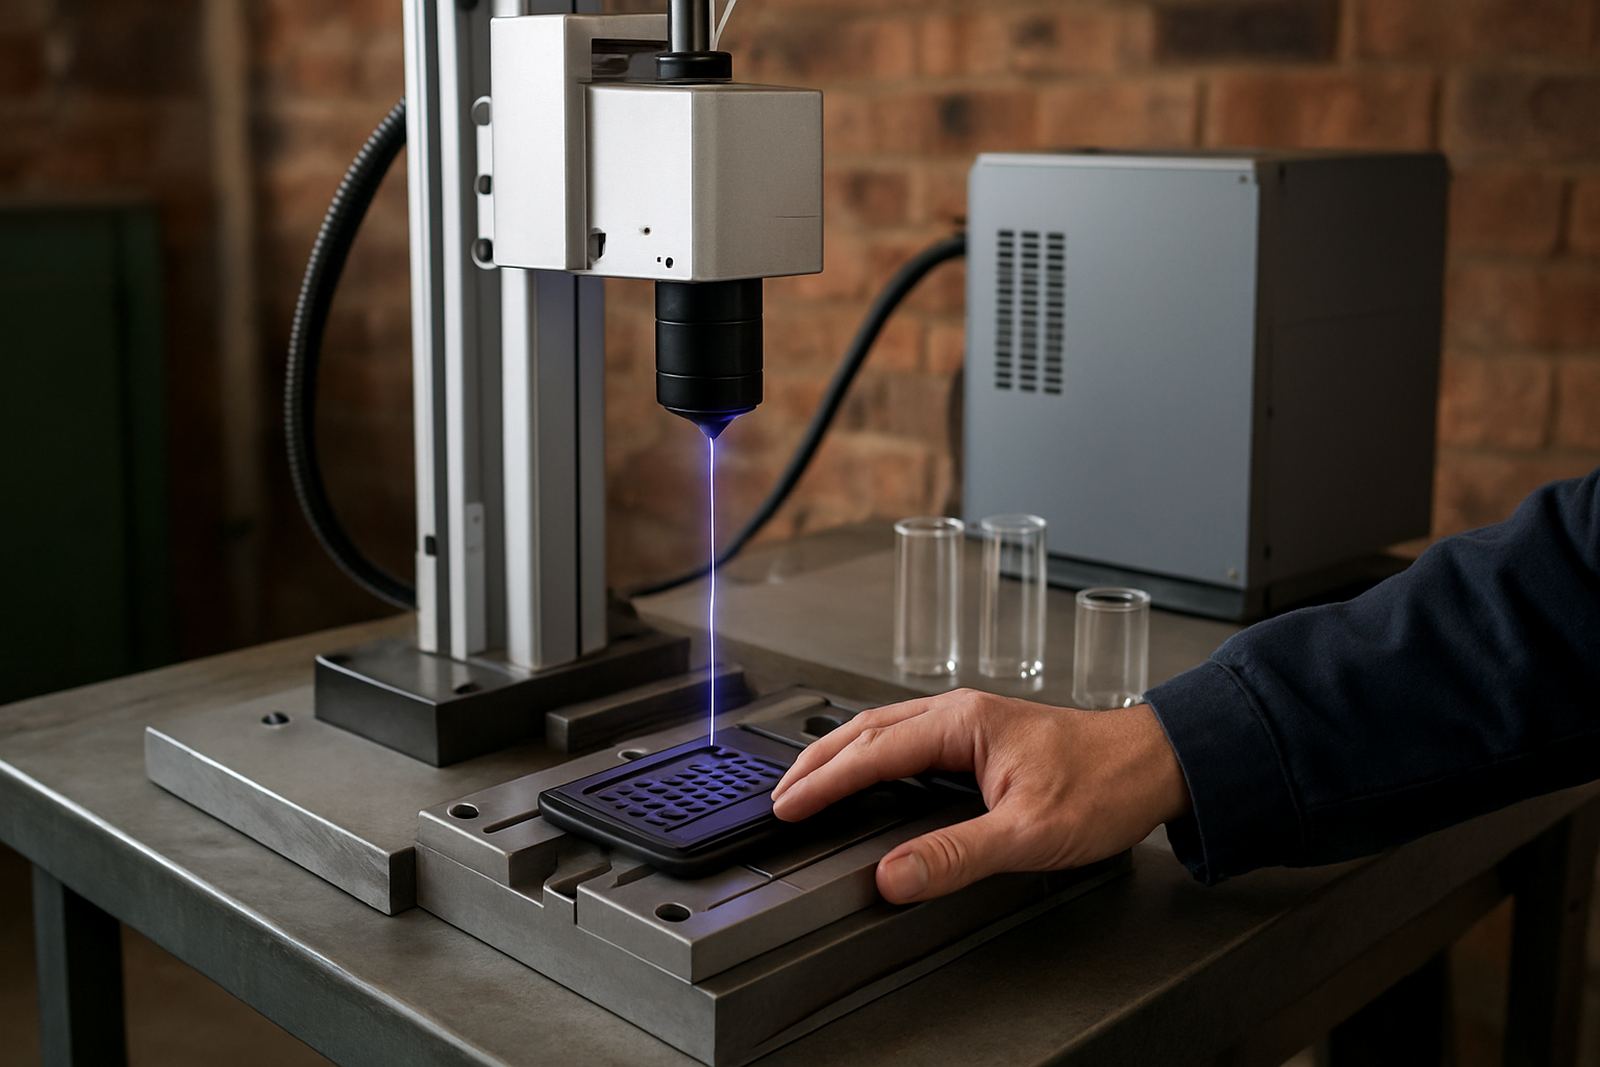
For plastic parts, permanent marking needs to be clear but controlled. UV laser marking is often used where the surface must stay clean and the code must not wear off. It is a good fit for many plastics because it can produce fine detail without stickers, inks or extra consumables. That matters in local factories where dust, heat and power interruptions can make consumable-based systems harder to manage.
Different plastics react differently to the marking process. Some give a bright contrast, while others need a different setting to bring the code into view. The right process is usually decided after sample testing, then fine-tuned for speed and readability. In areas like Alberton and Midrand, where production schedules are tight and floor space is limited, a well-set marking unit can be integrated into an existing line with very little disruption, provided the fixture and part handling are planned properly.
Permanent marking also helps with traceability. If a batch is moved between sites, stored in humid conditions or handled by different teams, the code stays where it should be. That is useful for quality control, returns and internal stock movement.
Readability depends on more than the code itself
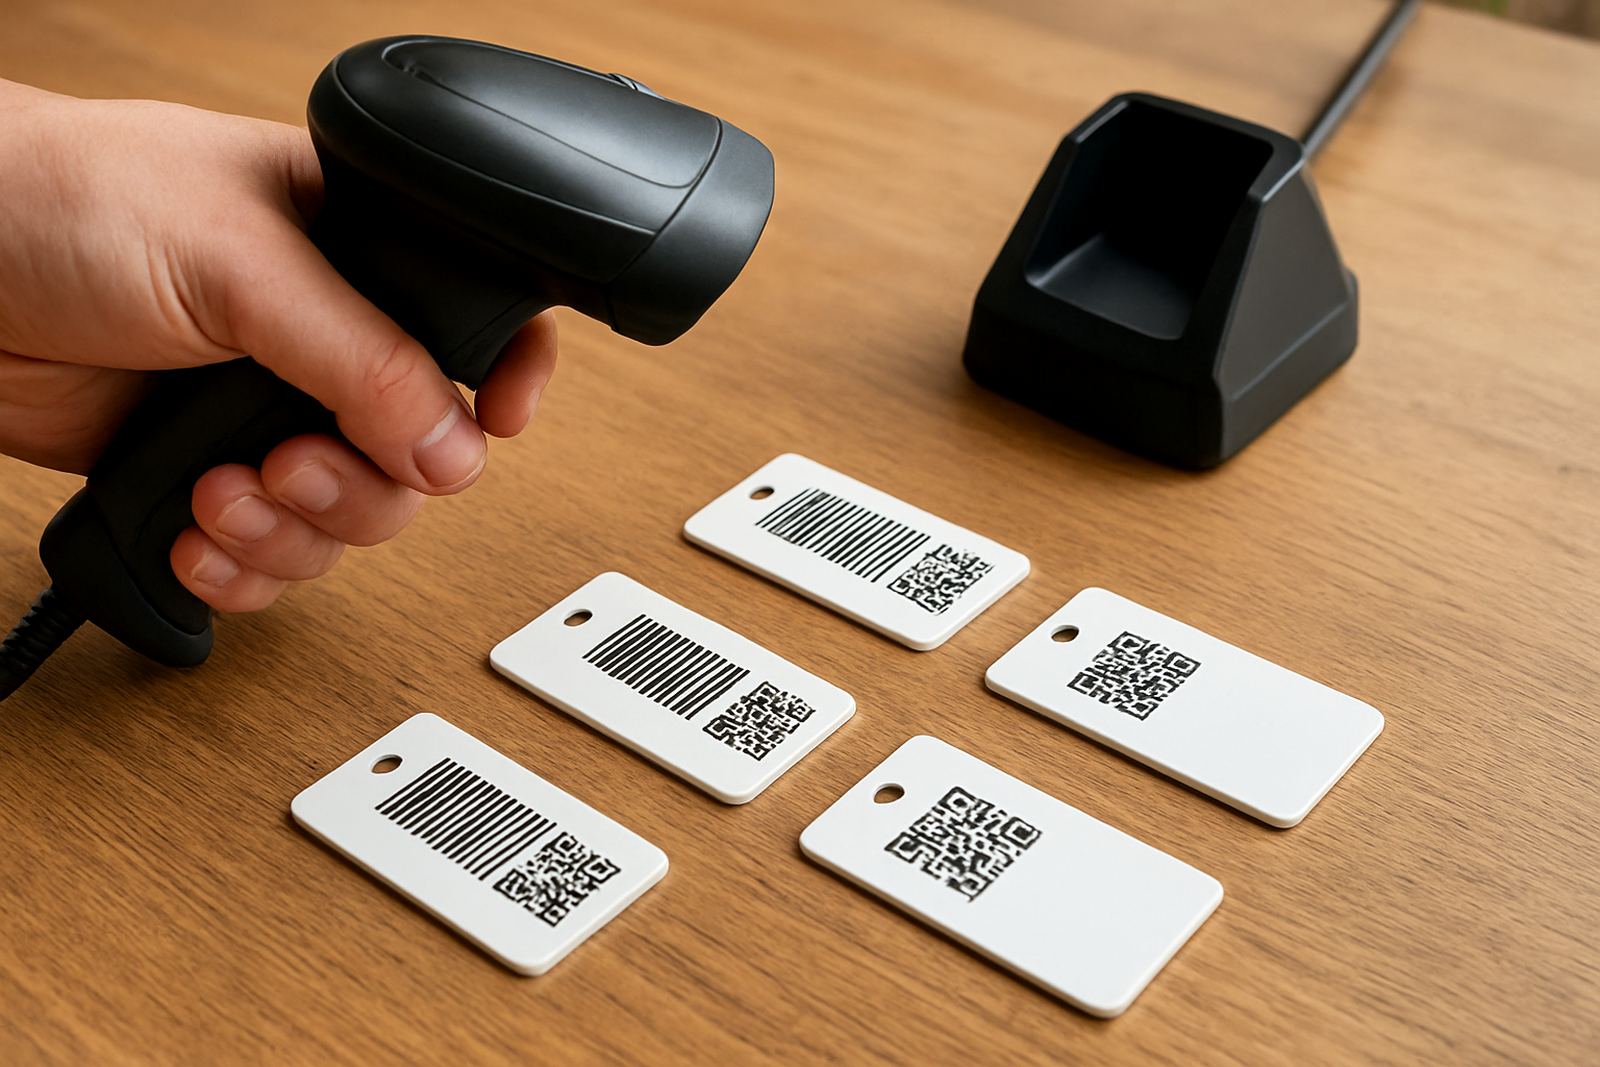
A barcode can be perfectly marked and still fail if the surface around it is not suitable. Gloss, dust, mould release residue and uneven part positioning can all interfere with reading. The scan quality also depends on lighting and the angle of presentation. For plastic components with shiny finishes, the mark may need to be placed where reflection is lower, or the scan station may need better control over the part orientation.
This is especially important in South African factories where production conditions can change through the day. Load-shedding, warm plant rooms and coastal humidity can all affect handling and inspection routines. If operators are rushing to keep up with an interrupted shift, the easiest code to read is usually the one that was planned properly from the start.
- Keep the mark away from high-gloss edges where glare can build up.
- Maintain a clear quiet zone around the bars and text.
- Use stable fixtures so each part is marked in the same position.
- Check readability after moulding, packing and any post-process cleaning.
A local example from a plastics line in Ekurhuleni
A plastics manufacturer in Ekurhuleni needed barcodes on small injection-moulded parts used in consumer assemblies. The first issue was not the marking itself, but the space available. The part had a curved face, a small logo panel and a raised edge close to the intended code area. After sample testing, the code was moved slightly lower and the character spacing was adjusted so the scanner could pick it up at normal speed.
The team also had to account for shift changes, so operator training was kept simple. The line staff only needed to check part position, confirm the code location and watch for any dirt on the fixture. Once the process was set, the marked parts held their readability through storage and packing. That kind of result is what matters on the floor, not a perfect looking sample that fails under daily use.
In situations like this, a site demo and sample testing save time. It is easier to adjust spacing, size and placement before a production run starts than to rework stock later. For companies in Boksburg, Germiston or Benoni, that practical step can prevent a lot of waste.
How to plan a barcode project on plastic parts
If you are planning barcodes on plastic, start with the part itself. Measure the available flat area, check the finish and note where the scanner will read from. Then test the mark on the actual material, not just a sample image. The goal is to make the code reliable in real use, whether the parts are moving through an internal warehouse or going out to a customer site.
It also helps to think beyond marking. If the part needs a fixture, line integration or software setup, plan that before installation day. A clean process is easier to maintain and less likely to break down when the team is under pressure. For businesses in Pretoria, Jet Park or across the East Rand, nationwide support and preventive maintenance can keep the system steady over time.
- Confirm the part material and finish before choosing the marking method.
- Allow enough quiet zone for reliable scanning.
- Test with the exact scanner type used on site.
- Build in operator training and simple daily checks.
- Plan for maintenance so readability does not slip over time.